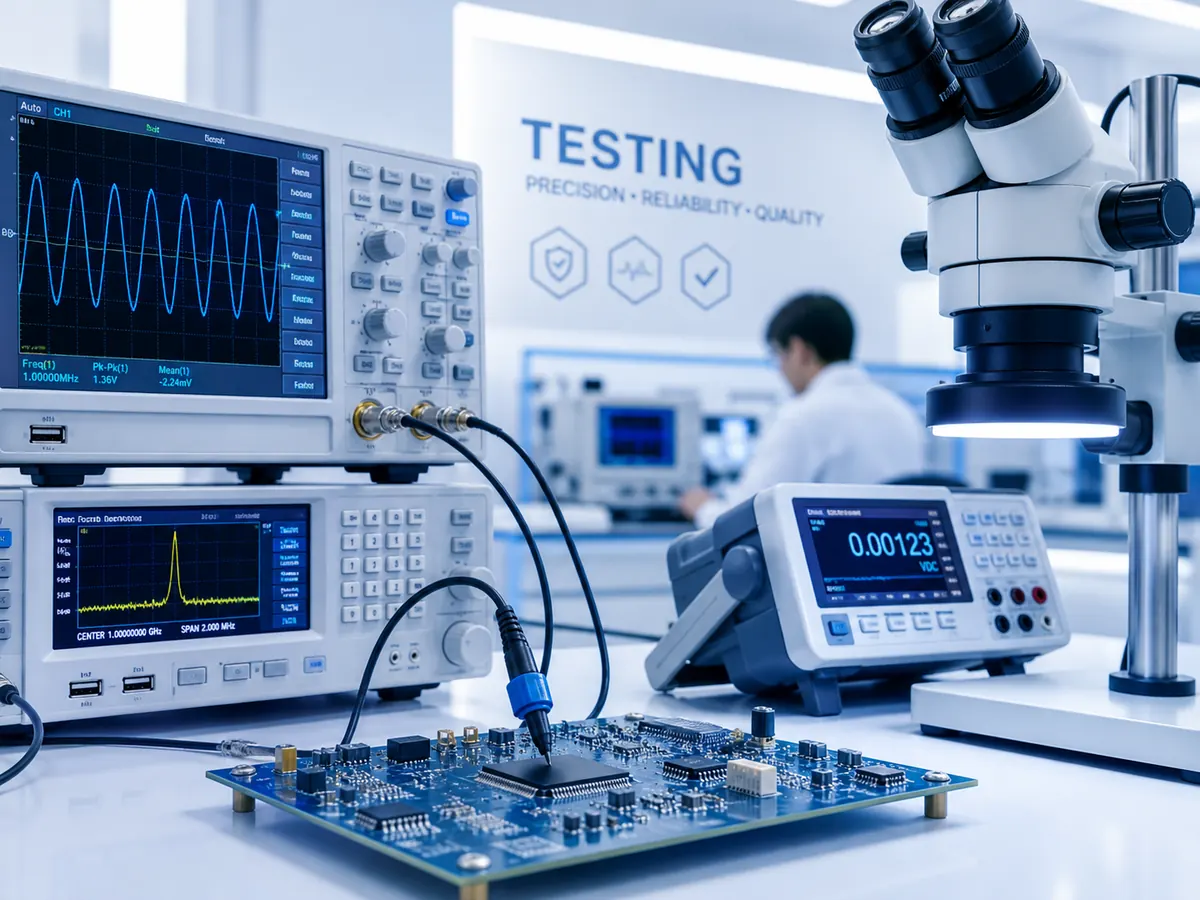
Navigating the complexities of international trade requires rigorous validation of product safety, performance, and regulatory adherence. Independent evaluation serves as the cornerstone of modern quality assurance, providing unbiased verification that products meet stringent international standards before they reach the market. This objective assessment not only safeguards consumers but also protects brand reputation and facilitates frictionless cross-border commerce.
Core Objectives of Independent Evaluation
Engaging an independent laboratory for product validation goes beyond mere checkbox compliance. It establishes a robust framework for quality assurance that permeates the entire product lifecycle. By leveraging external expertise, manufacturers and retailers can align their offerings with diverse regional mandates and consumer expectations.
Ensuring Regulatory Compliance
Different markets enforce distinct regulatory frameworks, such as CE marking in Europe, FCC regulations in the United States, and CCC in China. Independent laboratories possess specialized knowledge of these evolving legal landscapes. They conduct precise evaluations to verify that products satisfy all statutory requirements, thereby preventing costly market rejections, customs seizures, and legal liabilities.
Mitigating Supply Chain Risks
Global supply chains are inherently vulnerable to inconsistencies in manufacturing processes and raw material quality. External validation acts as a critical risk management tool. By identifying defects, material substitutions, or performance deviations early in the production cycle, businesses can prevent large-scale recalls and maintain uninterrupted distribution channels.
Key Testing Methodologies and Standards
A comprehensive evaluation program encompasses a wide array of scientific and technical procedures. These methodologies are designed to simulate real-world conditions and stress factors, ensuring that products can withstand their intended use environments.
| Testing Category | Primary Focus | Common Standards |
|---|---|---|
| Mechanical & Physical | Structural integrity, durability, and safety mechanisms | ISO, ASTM, EN |
| Chemical Analysis | Presence of restricted substances, toxicity, and material composition | REACH, RoHS, CP65 |
| Electromagnetic Compatibility | Interference, emissions, and electrical safety | FCC, CE-EMC, IEC |
| Environmental Simulation | Performance under extreme temperatures, humidity, and vibration | MIL-STD, IEC 60068 |
Physical and Mechanical Testing
This category evaluates the structural resilience and operational safety of products. Procedures include tensile strength assessments, drop tests, fatigue cycling, and load-bearing evaluations. For consumer electronics and automotive components, mechanical testing ensures that devices can endure physical shocks and prolonged usage without catastrophic failure.
Chemical and Environmental Analysis
Chemical analysis verifies that materials do not contain hazardous substances above permissible limits. Techniques such as X-ray fluorescence (XRF) and inductively coupled plasma mass spectrometry (ICP-MS) are utilized for precise elemental detection. Environmental analysis subjects products to controlled climatic chambers to assess their stability and functionality under varying thermal and moisture conditions.
Strategic Implementation in Quality Control
Integrating external validation into the quality control strategy requires a systematic approach. It is not a one-time event but a continuous process that adapts to production phases and market feedback.
- Design and Prototyping Phase: Conduct preliminary evaluations on initial prototypes to identify design flaws and verify that the conceptual engineering meets baseline safety and performance criteria.
- Pre-Production Verification: Validate the raw materials and initial production samples against approved specifications to ensure the manufacturing setup is correctly calibrated.
- During Production Inspection: Perform random sampling and in-line checks during the manufacturing process to monitor consistency and catch deviations before the entire batch is completed.
- Final Random Inspection: Execute comprehensive testing on finished goods packaged for shipment, confirming that the final output strictly adheres to the required quality benchmarks and packaging standards.
Data-Driven Continuous Improvement
Modern evaluation facilities provide detailed analytical reports that go beyond simple pass or fail results. These reports include trend analysis, root cause identification, and actionable recommendations. By leveraging this data, engineering and quality teams can refine manufacturing processes, optimize material selection, and drive continuous product enhancement.
Summary of Testing Imperatives
Independent validation remains an indispensable pillar for brands aiming to scale globally. It transforms subjective quality claims into objective, scientifically backed facts. By strictly adhering to international standards and implementing rigorous evaluation protocols, companies can confidently navigate diverse regulatory environments, minimize operational disruptions, and build enduring trust with consumers and stakeholders alike.
About Belling Global
Belling Global delivers integrated Testing, Inspection and Certification solutions to help businesses ensure compliance, reduce risk and strengthen supply-chain quality control for seamless access to global markets. Backed by state-of-the-art laboratory infrastructure and advanced analytical equipment, our technical team provides precise, reliable, and efficient evaluation services across multiple industries. We combine deep regulatory expertise with cutting-edge technology to deliver actionable insights that drive quality excellence.
Welcome to contact professional engineers for customized testing solutions and technical consultations.